The day’s percentage lands on the screen and someone asks whether the shift was good. Before you answer, you need to know what enters that number and what stays outside it. Overall equipment effectiveness (OEE) multiplies availability, performance, and quality; the EPA presents the index that way on its TPM page. The percentage summarizes a mix of losses. It is not a moral verdict on the shift.
English search results for “what is OEE” usually stop at the product of availability, performance, and quality. That framing is useful, and it is incomplete for a morning where the line kept running on temporary gear. The score can look fine while the designated asset sat isolated. What OEE does not count is whatever your local planned-time and stop rules leave out of the denominator.
This guide does not rebuild the formula step by step. The three-factor map is here to locate the gap. A bearing failure, a wheeled backup pump for a whole morning, and a preventive window that production blocked can leave the day’s OEE intact or even comfortable while the plant treats the morning as normal. The example numbers are hypothetical. They do not describe a real plant or an ROI.
If you already see a daily %, the useful work is to read which losses it captures and which decisions slip with no trace in the index. The figure alone is not enough to close the meeting. WizeeMind gathers plant evidence with source, time, and asset limits; it does not calculate official OEE or approve maintenance.
OEE as a loss map, not a grade for the day
OEE is a map of losses over a period, not a grade that passes or fails the morning. The EPA states that the index is calculated by multiplying, each as a percentage, overall equipment availability, performance, and the rate of quality products. Those figures orient you to how much time goes into each major loss and where to look next. EPA, Lean Thinking and Methods - TPM
JIPM presents Overall Equipment Efficiency (OEE) as a representative indicator of equipment efficiency, created during the development and diffusion of TPM, and notes that many companies use it today whether or not they have introduced TPM. It also mentions its appearance in IATF 16949 and in ISO 22400-2:2014. JIPM, About TPM
ISO 22400-1 offers an industry-neutral framework for defining, composing, exchanging, and using manufacturing operations indicators. It gives a view of what a KPI is, criteria for building one, and how to use it. It does not turn a daily percentage into an international benchmark or set a universal “good” threshold. ISO 22400-1:2014
When the meeting treats OEE as a grade for the day, the useful question disappears: which loss does each factor summarize, and which events sit outside the denominator? A shift can close high because the line produced acceptable units while a critical asset lived through an improvised bypass. The index is not lying if it was calculated under the local rule. It simply does not count what the rule does not include.
That shows up on shifts where everyone remembers the yellow cart and the report still closes “green.” The conversation sticks on the percentage and nobody opens the ticket for the isolated pump. The OEE map does not excuse that omission; it only shows the part of the ground the local definition lets in.
Before you compare shifts or plants, write down the period, the asset boundary, and which stops subtract from availability. The same definition logic appears when you compare plant performance when sites measure differently. Without that card, the percentage travels as if it were comparable, and it is not.
OEE does not replace stoppage analysis or the maintenance history. It helps you decide where to look. If the question is “why did it stop?” or “what got deferred?”, you need other evidence: timestamps, orders, photos of the bypass, a record of who blocked the preventive window. Without those annexes, the map reads as if the ground were clean.
Availability, performance, and quality on a plant shift
On a concrete shift, the three factors answer three different questions. Availability: how much of planned time was the line in a condition to produce under your rule? Performance: at what rate did it produce against the declared ideal cycle? Quality: what share of what was produced meets the acceptance rule? The EPA ties the index to those three rates so attention lands on the large equipment and process losses. EPA, Lean Thinking and Methods - TPM
NIST MEP documents a hydraulic press case at Keats: the system collected number of cycles, available current for production, and number of defective parts to calculate overall equipment effectiveness. Brian Keats, Quality Engineer, wrote that with TMAC the plant could track the overall efficiency of one of the most important stamping presses in the facility. NIST MEP, KEATS Hydraulic Press OEE System
That case also draws clear limits. The write-up lists qualitative results (better measurement accuracy, simpler quality entry, timely information for the maintenance plan) and states that a cost savings figure had not been developed. Do not treat that project as ROI proof or as a universal sensor template. NIST MEP, Keats case results
In the Lean and Six Sigma glossary, the EPA separates cycle time from takt: cycle time is the time for the standard sequence for one product (without queue time), and takt is available production time divided by customer demand. Mixing those clocks with OEE confuses three different timers. EPA, Appendix C
On the floor, a shift usually mixes short stops, changeovers, and spot defects. The EPA describes minor stoppage losses as frequent zero-to-ten-minute events that are hard to log by hand and often hidden in efficiency reports. It also describes speed losses when equipment slows to avoid defects or minor stops. EPA, equipment losses
ISO 22400-2 specifies a set of KPIs used in manufacturing operations, presented with formula, elements, time behaviour, and other characteristics, referenced to work units under IEC 62264. Having a definition standard does not mean your daily report uses those exact boundaries. ISO 22400-2:2014
If the committee wants a single number, say it with the map. Low availability points to time lost under the rule. Low performance points to rate. Low quality points to rejects or rework. No factor alone proves the cause. Soft performance with high availability does not prove a maintenance problem; it may be a misdeclared ideal cycle or uncaptured minor stops. Reading the index before a committee is a reading job, not a cosmetic one.
The morning that never shows up: pump, bearing, and wheeled backup
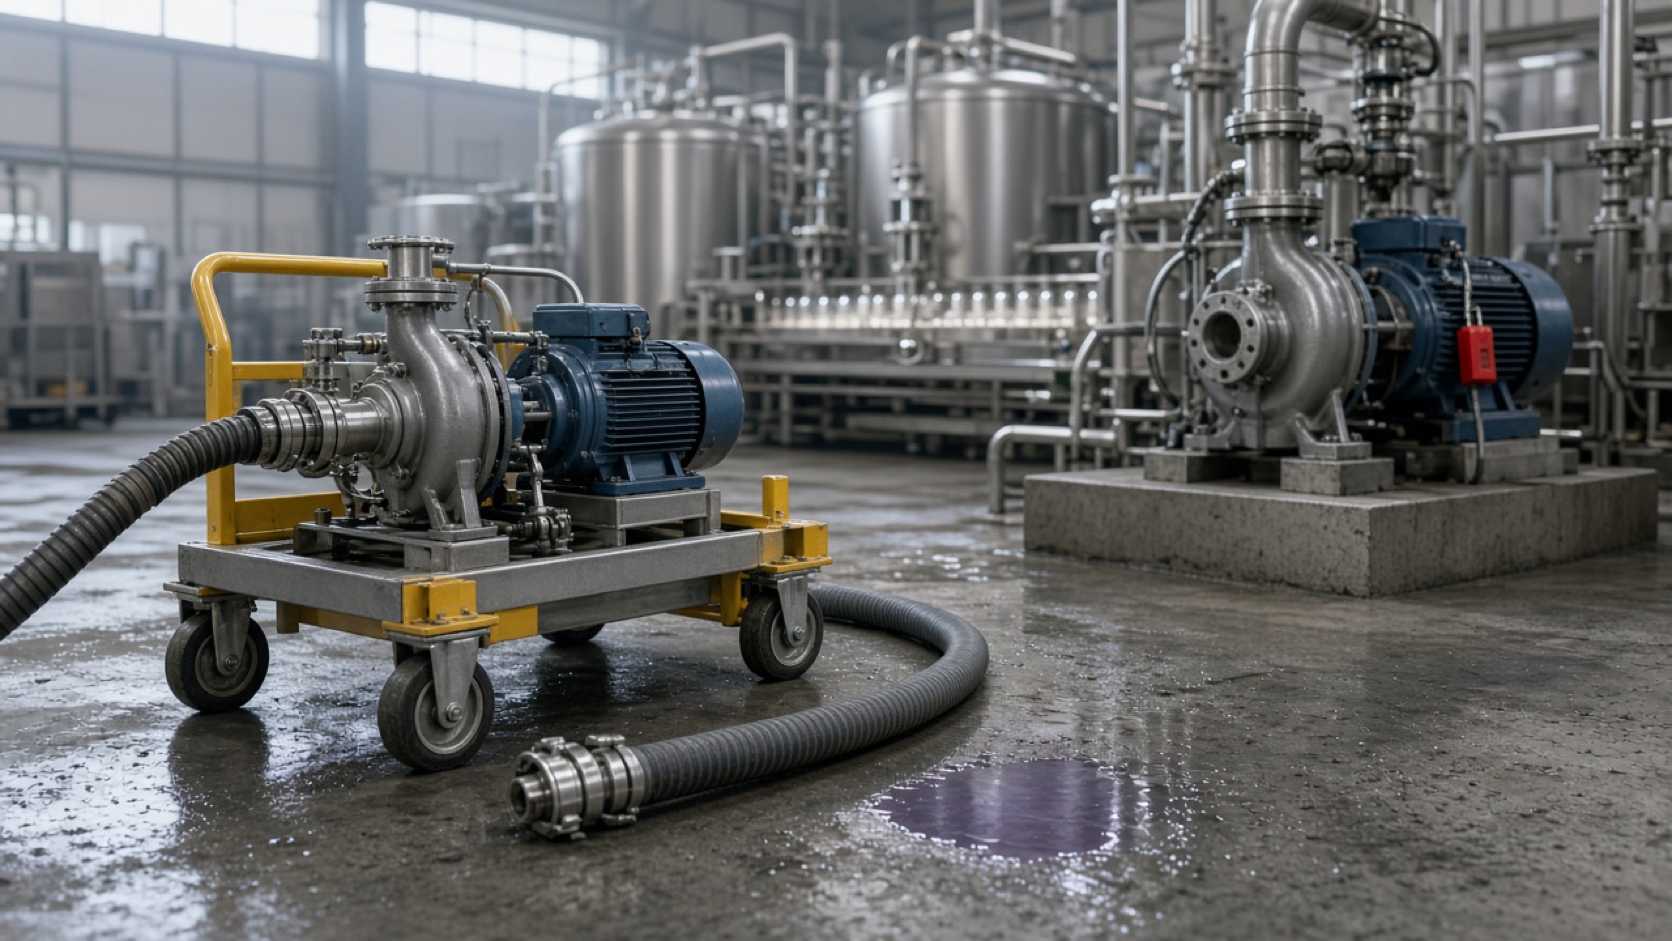
Picture a hypothetical scenario. At 06:40 the bearing fails on the installed transfer-line pump. This is not maintenance advice and not a real diagnosis; it is a story to show the indicator gap. Production rolls a wheeled backup pump onto a cart, connects temporary hoses, and the line starts sending product again. For four hours the plant “keeps going.” Someone says the shift was saved. By midday, OEE shows no collapse.
Why? Because many local availability definitions watch whether the line produced in planned time, not whether the designated asset was in service. If the denominator is “planned line time” and the numerator is “time the line produced,” the bypass may not subtract. The bearing failure stays in the maintenance history, in photos of the cart, and in the noise of the hoses. It does not necessarily land in the day’s availability factor.
In that scenario, the critical asset is isolated and flow depends on a temporary setup. The percentage watcher sees continuity. The floor watcher sees hoses, a cart, and a fixed pump out of service. Both readings can be true at once if the indicator rule does not force a subtraction for the bypass. The uncomfortable part is that neither person is inventing data; they are looking at different clocks.
The EPA classifies unexpected breakdown losses as equipment downtime for repairs, with costs that can include downtime, lost production opportunity, labor, and spare parts. EPA, unexpected breakdown losses In the hypothetical scenario, part of that cost shifts: the line does not stop fully, but the critical asset is isolated and the operation depends on a temporary setup.
HSE reminds that plant and equipment maintenance is done to prevent problems, correct faults, and make sure equipment works effectively; it can be a planned programme or short-notice work after a breakdown, and it always involves non-routine activities with risks. HSE, Maintenance of work equipment An improvised bypass is not “the day saved” in risk terms; it is a different mode of operation. The day’s OEE may not show it.
Douglas Thomas, in NIST AMS 100-18, describes reactive maintenance as what happens when the manufacturer leaves machinery until it breaks or needs repair, against preventive and predictive approaches. NIST AMS 100-18 The wheeled-pump scenario fits that operating logic: action starts when the failure has already happened. That does not mean the shift OEE must be low; it means the index and the failure mode are not telling the same story.
To keep the trail, record the isolated asset, failure time, bypass in-service time, who authorized the setup, and what was deferred. Downtime analysis with operational evidence and line stoppage analysis in minutes help keep timestamps even when the day’s percentage looks “normal.”
The preventive work that production blocked
Same hypothetical morning, another layer. There was a two-hour preventive window on the installed pump: lubrication, checks, and a planned element change in the low-demand slot. Production blocked the window because “we cannot stop now” and because the wheeled backup already held the flow. The work was deferred. At the end of the shift, OEE can still look high. The line produced. Performance did not collapse. Quality did not move in the report.
The percentage does not record the deferral. What stays outside is the unfinished task, the risk that stacks up, and the dependence on the bypass. Bring only the % and you can call the day acceptable. Bring the deferred order and the conversation changes.
HSE states that an effective maintenance programme makes equipment more reliable, that fewer breakdowns reduce dangerous contact with machinery, and that PUWER requires work equipment to be maintained in an efficient state, in efficient working order, and in good repair. HSE, why maintenance matters
Production pressure is real. So is the quiet cost of living on temporary hoses for another shift because the window slipped again.
This page is not safety advice for your jurisdiction. HSE writes from the Great Britain framework. Your plant still sits under local equipment duties and approved procedures. Deferring preventive work can be an explicit operating decision. It should not be confused with “OEE says the day was good.”
The EPA places TPM in breakdown prevention, daily autonomous maintenance (checks, lubrication, simple parts replacement, anomaly detection), and loss elimination. EPA, TPM and autonomous maintenance If the preventive window is cancelled with no record, the daily index does not replace the plan.
NIST AMS 100-18 examines costs and losses across maintenance techniques and warns about limited national-scale understanding of those costs and of the data needed to estimate them. NIST, costs and benefits of advanced maintenance Do not invent an ROI for the deferred preventive work. Write down what was deferred, who decided, and what condition would make continuing on the bypass unacceptable.
The choice among predictive, preventive, and corrective is covered in more detail in predictive, preventive, or corrective maintenance and in maintenance troubleshooting with plant evidence. Here one reading rule is enough: if the preventive work did not happen, the day’s OEE will not shout it for you.
Short calculation: plug in your hours and see what stays out
This section is a hypothetical example with reproducible arithmetic, plus a blank template. It is not a universal formula for “hidden hours.” Which hours enter or stay out depends on the local definition of planned time, of stops that subtract from availability, and of asset boundaries. The EPA gives the product-of-factors structure; it does not fix one denominator for every plant. EPA, OEE calculation
Hypothetical shift assumption (eight planned line hours):
- Planned time: 8.00 h
- Stops that do subtract from availability under the local rule (logged material shortage): 0.50 h
- Line operating time: 7.50 h
- Illustrative availability: 7.50 / 8.00 = 0.9375 (93.75 %)
- Illustrative performance: 0.95
- Illustrative quality: 0.98
- Illustrative OEE: 0.9375 × 0.95 × 0.98 ≈ 0.873 (87.3 %)
Now the hours that, in this assumption, do not subtract from the availability factor:
- Wheeled backup (bypass) hours: 4.00 h
- Deferred preventive hours: 2.00 h
Example OEE remains ~87.3 %. The four bypass hours and the two deferred preventive hours do not appear in the product if the local rule only subtracts logged line stops. That does not prove the day was good. It proves the index and the operating morning are not the same story.
If your plant already subtracts bypass time, say so in the definition card and the arithmetic will look different. The point of the worksheet is the gap your own rule creates, not a universal hidden-hours tax.
Blank template (fill only with your local definitions):
- Planned time (h): ______
- Stops that do subtract from availability (h): ______
- Resulting operating time (h): ______
- Availability = operating / planned: ______
- Performance (fraction): ______
- Quality (fraction): ______
- OEE = availability × performance × quality: ______
- Bypass hours your rule does not subtract: ______
- Deferred preventive hours not subtracted: ______
NIST MEP shows that OEE depends on a concrete data chain (cycles, availability to produce, defects). If you change the “available to produce” boundary, the factor changes even when the formula keeps the same name. NIST MEP, OEE data capture
ISO 22400-2 presents KPIs with formulas and associated elements; it does not turn your template into a plant standard. ISO 22400-2:2014 Declare period and bases before you multiply.
Concrete next step: take the last shift, write the two “hours that do not subtract” rows, and bring them to the meeting with the %. If those rows are empty because nobody records them, the problem is not OEE. It is the missing evidence. A well-calculated index with a narrow boundary is still a narrow index.
If you want the calendar time that never enters the OEE denominator, that reading is in TEEP: the calendar that the OEE leaves out.
Frequently asked questions
What is OEE in one useful plant sentence?
OEE is the product of availability, performance, and quality over a declared period; it summarizes different losses and does not certify that the day was good. The EPA calculates it by multiplying those three percentage rates. EPA, OEE definition JIPM places it as a representative equipment-efficiency KPI diffused with TPM. JIPM, OEE
Does a wheeled backup pump that keeps the line running count as good availability?
Only if your local definition treats that asset and that time as intended operation. If the installed pump is isolated and production continues through a bypass, the percentage may not register the problem. The EPA describes unexpected breakdowns as stops with downtime and lost-opportunity costs; a bypass can shift that cost outside the factor. EPA, breakdown losses HSE stresses planning maintenance and the risks of non-routine work. HSE, maintenance
Does deferred preventive work blocked by production worsen the day’s OEE?
Not necessarily. If the line keeps producing, the deferred task may not subtract from availability even though operating risk has grown. PUWER, in the framework HSE describes, requires work equipment to be maintained in an efficient state and in good repair; deferral does not erase that duty in that jurisdiction. HSE, PUWER and maintenance NIST distinguishes reactive, preventive, and predictive maintenance when it examines costs and losses. NIST AMS 100-18
Is there a universal formula for hidden hours outside OEE?
No. Which hours enter or stay out depends on the local definition of planned time, of stops, and of asset boundaries. There is no single hidden denominator for every plant. ISO 22400-1 frames how KPIs are defined and used without imposing a universal daily threshold. ISO 22400-1 ISO 22400-2 details KPIs with formulas and elements; the operating boundary remains a documented decision. ISO 22400-2
Can OEE alone decide maintenance without other evidence?
No. The index points to which loss to inspect; it does not replace failure records, deferred work orders, or safe maintenance criteria. The Keats case from NIST MEP shows capture of cycles, availability, and defects to calculate OEE, with no published savings figure on that page. NIST MEP, Keats The EPA keeps OEE separate from metrics such as takt and cycle time. EPA, Appendix C